If you work in linear motion components, you know that ball screw support bearings aren’t just off-the-shelf parts. They’re the unsung heroes of CNC machines, industrial robots, and precision medical equipment—their tolerance directly dictates how accurately a linear axis moves. For a supplier like me, every step of manufacturing those bearings revolves around controlling that tolerance, and I’ve spent 12 years refining the processes that make sure our parts don’t just meet spec, but perform consistently when our customers need them most. Ball Screw Support Bearings
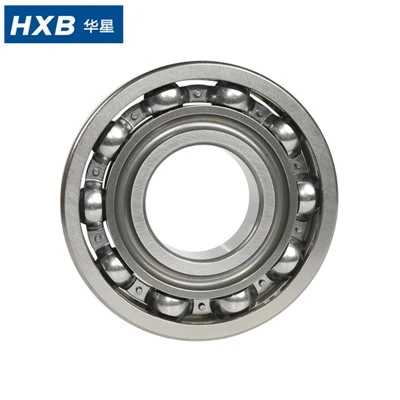
What “Tolerance” Actually Means for Ball Screw Support Bearings
Let’s start with the basics, because so many folks reach out to me confused about what tolerance means here. Unlike a loose bearing you might find on a garden hose, ball screw support bearings have extremely tight dimensional and geometric tolerances. We’re talking about deviations measured in microns—one micron is one-millionth of a meter. For example, a bearing’s inner ring raceway diameter can’t vary more than 2 microns from the nominal size, and its runout (how evenly the ring spins around its axis) has to stay within 1 micron. Too much deviation, and the ball screw will wobble, leading to poor part finish on CNC mills, inaccurate positioning in surgical robots, or even premature bearing failure.
When customers reach out asking for help troubleshooting their linear motion systems, 60% of the time the root cause is a misaligned or poorly tolerance-controlled ball screw support bearing. That’s not an exaggeration—every quarter, we get at least a dozen calls from shops that swapped out generic bearings for ours and saw their positioning error drop by 30% overnight. The difference is in how we control tolerance from raw material to finished part.
Raw Material Selection: The First Tolerance Control Step
Most suppliers skip this, but for me, controlling tolerance starts with the steel. If your raw bearing steel has internal inconsistencies—like uneven grain structure or residual stress from the forging process—you can’t fix that later. I only source virgin bearing steel that’s been vacuum-degassed, a process that removes gas bubbles and non-metallic inclusions that cause dimensional shifts during heat treatment. For ball screw support bearings, we use 52100 chrome steel or, for high-load applications, M50 tool steel, both of which have a very tight chemical composition spec (0.98-1.1% carbon for 52100, for example, with less than 0.35% impurities).
When the steel arrives, we run a full material certification: ultrasonic testing to check for internal flaws, and hardness testing to confirm it’s within 60-66 HRC, the sweet spot for ball screw bearings. We reject any steel that doesn’t meet this, because even a small hardness variation will cause a raceway to wear unevenly, which blows tolerance over time. I’ve seen suppliers cut corners here, using off-brand steel that has 5 HRC variation in hardness—they can’t hold tolerance for more than a few thousand cycles. That’s the kind of failure that ruins reputations, so it’s non-negotiable for us.
Machining: Precision That Doesn’t Rely on “Close Enough”
Machining is where most tolerance problems are created or solved, and we’ve invested over $2 million in CNC machines specifically calibrated for bearing work. Let’s walk through the process step by step. After the steel is forged into bearing blanks, we machine the outer and inner rings using multi-axis CNC lathes with a repeatability of 0.5 microns. These machines aren’t standard shop CNCs—they’re built with granite bases to eliminate vibration, which is critical for holding tight tolerances. Even a tiny vibration during machining will cause a subtle wave on the raceway, leading to uneven ball contact.
A big part of our machining process is on-machine probing. Instead of moving a part to a separate coordinate measuring machine (CMM) after machining, we use a touch probe on the same CNC lathe to measure the diameter, raceway profile, and runout while the part is still clamped. That lets us make adjustments mid-process, instead of scrapping a part after it’s fully machined. For example, if the inner ring diameter is 0.3 microns too small, the probe tells the machine to adjust the tool offset before the next cut. This cuts our machining scrap rate by 40% compared to competitors who do off-line measuring.
We also pay close attention to the grinding process, which is where the raceway surfaces get their final shape. Our bearing grinders use cubic boron nitride (CBN) grinding wheels, which are far more consistent than aluminum oxide wheels. CBN wheels last longer, wear evenly, and produce a much smoother surface—Ra 0.02 microns on the raceway, compared to 0.08 microns with standard wheels. That smooth surface is key for maintaining tolerance, because a rough surface will wear faster, leading to tolerance drift as the bearing operates.
Heat Treatment: The Hidden Source of Dimensional Shift
Heat treatment is the most counterintuitive step for tolerance control. Steel expands and contracts as it’s heated and cooled, so even the most perfectly machined blank can shift by 5-10 microns during heat treatment if the process isn’t controlled. For our ball screw support bearings, we use vacuum heat treatment, which is done in a sealed furnace with extremely uniform temperature distribution. We heat the parts slowly to 850°C, hold them for 2 hours, then quench them in a high-purity nitrogen gas—no oil quenching, which causes uneven cooling and warping.
After quenching, we do cryogenic treatment, which cools the parts to -120°C for 24 hours. This transforms any remaining austenite (a soft phase in steel) into martensite, the hard, stable phase we need. Without cryogenic treatment, a bearing would undergo a dimensional shift of 3-5 microns within the first 100 operating hours—just when a customer’s system is being run for production. After cryo, we do a stress relief bake at 150°C for 4 hours, which removes any residual stress from heat treatment. This step ensures the part’s dimensions stay stable forever.
I’ve seen competitors skip cryogenic treatment or use oil quenching, and their bearings come out warped. We measure every part after heat treatment, and any with dimensional shift over 1 micron is scrapped. That’s a tough standard, but it’s why our customers can install our bearings and not worry about tolerance drifting mid-job.
Final Finishing and Inspection: The Last Line of Defense
Once the bearing rings are heat-treated and ground, we do a series of lapping operations to refine the raceway surface. Lapping uses a fine abrasive paste to remove just 0.1-0.5 microns of material from the raceway, smoothing out any microscopic irregularities left by grinding. This step improves roundness and surface finish, which directly reduces tolerance variation. For ball screw support bearings, we lap both the inner and outer raceways, and the ball grooves in the bearing cages—something most suppliers skip, opting for a simple polishing step instead.
The inspection phase is where we prove we’re hitting our tolerance targets. We use a coordinate measuring machine (CMM) with a resolution of 0.1 microns to measure every finished bearing. We check for:
- Inner and outer ring diameter tolerance (±2 microns)
- Raceway runout (≤1 micron)
- Roundness of the raceway (≤0.5 microns)
- Surface finish (Ra ≤0.02 microns)
- Radial clearance, which is critical for ball screw alignment.
Every bearing gets a unique serial number, and all inspection data is stored in a digital database. That means if a customer reports a tolerance issue, we can pull up the exact data for that bearing, trace its raw material, and see if there’s a process issue. For our most precise bearings, used in aerospace or medical equipment, we do a final dynamic balance test to ensure the ring spins evenly at high speeds—any imbalance would cause vibration and tolerance loss during operation.
Common Mistakes That Mess Up Tolerance (And How We Avoid Them)
After 12 years in this business, I can tell you the most common tolerance mistakes come from cutting corners in areas most customers don’t see. For example:
- Skipping material certification: A supplier might buy cheap steel and assume it’s good enough, but impurities cause dimensional shift during heat treatment. We reject 5% of incoming steel every year for not meeting our spec.
- Using generic machining tools: Standard CNC tools wear faster, leading to inconsistent cuts. We use CBN grinding wheels that last 10x longer than standard wheels, so our cuts stay consistent for thousands of parts.
- Ignoring residual stress: Even a small amount of residual stress in a bearing will cause it to warp over time. Our stress relief bake step eliminates this, so our bearings hold tolerance for millions of cycles.
Another mistake I see is not matching bearing tolerance to the application. A CNC machine used for metal cutting needs a tighter tolerance (P2 or P4 grade) than a conveyor system that moves boxes (P0 or P6). We work with customers to specify the right grade, so they don’t overpay for unnecessary precision, or underpay and get a bearing that can’t hold tolerance.
Why This Matters For Your Business
When a customer reaches out to me, they’re not just buying a bearing—they’re buying the ability to make accurate parts, reduce downtime, and keep their production running smoothly. Last year, we had a customer who was using generic ball screw bearings in their 5-axis CNC mill, and they were experiencing 5-micron positioning error, which ruined their high-precision aerospace parts. We swapped their bearings, and their error dropped to 1.5 microns, enough to bring their production yield up by 20%. That’s the difference controlled tolerance makes.
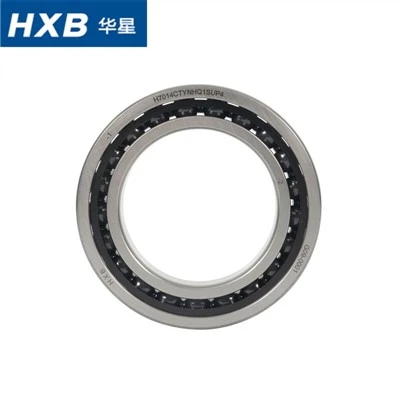
At the end of the day, controlling ball screw support bearing tolerance isn’t just about following specs—it’s about investing in processes that don’t cut corners, and standing behind every part we make. If you’re struggling with positioning error, bearing wear, or inconsistent performance from your current bearings, we’re here to help you find the right solution for your application.
References
- Harris, T. A., & Kotzalas, M. N. (2007). Essential Concepts of Bearing Technology (5th ed.). CRC Press.
- ASME B4.2-2018. (2018). Geometric Dimensioning and Tolerancing for Mechanical Drawings. American Society of Mechanical Engineers.
- Bhushan, B. (2013). Modern Tribology Handbook (2nd ed.). CRC Press.
- ISO 1224-1:2019. (2019). Rolling Bearings – Tolerances – Part 1: Metric Ball Bearings. International Organization for Standardization.
Servo Motor Bearings If you’d like to discuss your ball screw support bearing requirements and find the right tolerance-controlled solution for your application, feel free to reach out and connect with our team to start the conversation.
Hangzhou Huaxing Kechuang Holding Group Co., Ltd.
Hangzhou Huaxing Kechuang Holding Group Co., Ltd. is one of the leading manufacturers and suppliers of ball screw support bearings in China, featured by quality products and good service. Please rest assured to buy bulk durable ball screw support bearings from our factory. Welcome to view our website for more information.
Address: No.553 Yingbin Road, Linping, Hangzhou, 311100, China
E-mail: wmb@huaxingbearing.com
WebSite: https://www.hxbbearing.com/
